Hey everyone, let’s cut the crap—when you’re sourcing threaded valves, the last thing you want is a part that fails mid-install or worse, leaks on the job site. As someone who’s been in the threaded valve game for over a decade, I’ve seen it all: folks skipping basic tests, cutting corners, and ending up with way more headaches than they bargained for. Today, I’m breaking down exactly how we test every threaded valve that leaves our shop—no fancy jargon, just real steps that actually work. Threaded Valve
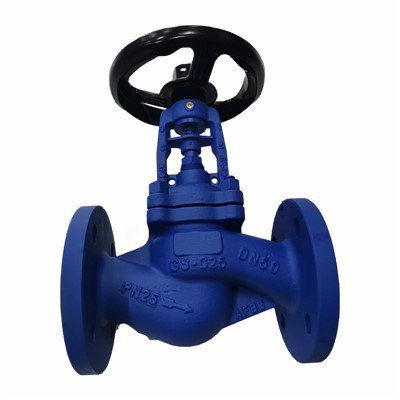
First off, let’s get one thing straight: threaded valves aren’t one-size-fits-all. They get used for everything from residential plumbing to industrial chemical lines, so your testing can’t be generic. Back when I started, we’d just slap a valve on a pipe, pump some water, and cross our fingers. Yeah, that worked for low-pressure stuff, but the first time a client’s high-pressure steam line burst because we missed a tiny thread defect, we learned real quick that approach was garbage. Now? We follow a step-by-step process that checks every single thing that could go wrong with a threaded valve, starting with the part that makes it a threaded valve in the first place—the threads.
Wait, I know what you’re thinking: threads are cut, right? Why test them? Oh, man, have you seen cheap imports with burrs, cross-threaded cuts, or even half the threads missing? That’s a disaster waiting to happen. A valve with bad threads won’t seal properly, no matter how tight you wrench it. Our first test for every valve is a thread inspection—we don’t just eyeball them. We use thread gauges, like the tapered plug gauges for NPT (National Pipe Thread) because that’s what most folks use, but if it’s BSPT or whatever, we match the gauge. We run the gauge over both the male end (the valve’s threaded shank) and the female end (the fitting it connects to) to make sure the pitch, taper, and thread depth are exact. No exceptions. If a thread is even a hair off, that valve gets tossed. I don’t care if it’s a $5 part or a $500 part—bad threads are non-negotiable. Last month we had a client send back 20 valves because their installer couldn’t thread them, turns out the import we tested once missed that the female threads were cut 1/32” too shallow. We ate the cost, fixed our process, and now we do a 100% thread gauge check instead of sampling. That’s the kind of stuff that keeps clients coming back.
Next up, pressure testing. This is the big one—if a valve leaks when it’s supposed to hold pressure, it’s useless. But wait, there’s a right way and a wrong way to pressure test a threaded valve. A lot of guys just hook it up to a water line, crank the pressure, and wait 10 minutes. No, that’s not enough, especially for different types of valves. We categorize valves first: gate valves, ball valves, globe valves, check valves—each has its own pressure specs. For example, a 2-inch 150# threaded ball valve isn’t tested the same as a 1-inch 300# gate valve. Here’s how we do it: first, we seal both ends of the valve (we use custom threaded caps that match the valve’s size, so we don’t damage the threads from gluing or welding stuff on). Then, we fill the valve completely with deaerated water—no air bubbles. Air in the system will make pressure readings wonky and can even cause the valve to fail because of hydraulic shock. Once it’s full, we pressurize it to its rated working pressure, hold it for 1 minute, then bump it up to 1.5 times the rated pressure (that’s the hydrostatic test pressure, for the folks keeping score at home) and hold it for 5 minutes. During that time, we do a visual check for leaks—any seepage, even a tiny drip, and the valve is out. We also check for thread movement: if the valve’s body twists when we pressurize it, that means the thread connections were flawed, and it’ll leak when installed. We mark those ones as “for scrap” immediately. Oh, and don’t forget about vacuum testing for valves that get used in negative pressure systems—like industrial suction lines. We’ll pull a 29-inch mercury vacuum on the valve for 10 minutes, and if the vacuum drops more than 1 inch, that’s a fail. I’ve seen ball valves pass pressure tests but flunk vacuum because their seat was misaligned—you can’t skip that step.
Wait, what about the valve’s internal parts? Threaded valve bodies are usually made of brass, cast iron, stainless steel, or maybe plastic for low-pressure stuff. We need to make sure there are no defects in the casting or manufacturing that would cause the valve to malfunction. That’s where non-destructive testing (NDT) comes in, but again, we keep it real—no fancy $100k X-ray machines unless it’s for super high-pressure industrial valves. For most of our stock, we use dye penetrant testing. We spray a penetrant liquid on the valve body, let it sit for 10 minutes so it seeps into any tiny cracks, porosity, or voids, then wipe it off and spray a developer. Any defect will show up as a bright spot on the developer, and those valves get scrapped. For stainless steel valves that might be used in corrosive environments, we also do a magnetic particle test to check for surface and subsurface cracks. Yeah, it’s a little extra work, but last year we caught a porosity defect in a batch of brass gate valves that would’ve corroded and leaked within 6 months. Instead of dealing with a return, we fixed the issue before the valves left our shop.
Another thing most people overlook: functional testing. A valve might look good, pass pressure, have good threads, but if it won’t open or close all the way, what’s the point? Functional testing is straightforward, but we do it for every single valve. For manual valves, we operate the handle or wrench multiple times—full open, full closed, and a couple of positions in between—to make sure there’s no binding, sticking, or excessive play. For ball valves, we make sure the quarter-turn is smooth and stops exactly at open or closed; if it’s sloppy, the stem seal will leak. For gate valves, we check that the gate doesn’t get stuck halfway, which would mean partial flow and possible damage to the seat. For check valves—those one-way valves—we test both directions: apply pressure from one side, make sure it holds, then apply from the other side, make sure it opens and lets flow through. I had a client once who put in a bunch of check valves that wouldn’t close all the way, causing backflow that ruined their pump. We tested those valves before shipping, caught the ones with bad spring tension, and the client never had that problem again. Functional testing isn’t just about making sure the valve works—it’s about making sure it works as intended, which saves everyone time and money down the line.
Oh, and let’s talk about thread sealant compatibility? Wait, no, actually—we don’t test sealant, but we do make sure that our valves work with the sealant our clients are using. But here’s a pro tip: when installing threaded valves, the sealant shouldn’t go into the valve’s internal passages, right? That’s why we make sure the threads on the valve are flush with the end of the valve body, so when you wrap Teflon tape or use pipe dope, you don’t get gunk in the valve. Wait, is that part of testing? Kind of—we check the thread flushness during our visual inspection. If the threads stick out too far, they’ll cause a gap when you connect the fitting, leading to leaks. If they’re recessed too far, you won’t get a good bite on the fitting. We measure that with a caliper, so every valve has the right thread protrusion. That’s a small thing, but it’s the difference between a easy install and a call back.
Let’s not forget about cryogenic or high-temperature valves? If you’re using a threaded valve for a LNG line that’s -200°F, or a steam line that’s 500°F, standard pressure tests won’t cut it. We do temperature cycling tests for those valves—we freeze them down to their minimum operating temp, cycle them between hot and cold multiple times, then retest pressure. That checks for any thermal expansion or contraction that could cause cracks in the body or seat. We had a client in the energy sector who needed valves for a cryogenic application, and we tested their valves through 50 temperature cycles, which caught a tiny crack in the seat that would’ve failed after just a few uses in the field.
Now, let’s get real about common mistakes people make when testing threaded valves. First, sampling. A lot of suppliers will test 1 out of 100 valves and call it good. That’s garbage. We do 100% testing on all our stock valves, especially the critical ones. Why? Because even a perfect batch can have a bad part. I’ve seen batches of 500 valves where one slipped through the manufacturing line with a cracked body—if we’d only sampled, that one would’ve gone to a client and caused a problem. Second, rushing the pressure test. If you only hold pressure for 1 minute, a tiny leak won’t show up. We always hold for the full time, because leaks are slow sometimes, especially at lower pressures. Third, skipping thread inspection. Like I said earlier, bad threads are the #1 cause of threaded valve failures. Don’t just eyeball them—use a gauge. That’s non-negotiable. Fourth, ignoring corrosion resistance. If your valve is going in a saltwater line or a chemical plant, a pressure test at room temp won’t tell you if the body will rust or corrode. We do salt spray testing for stainless and brass valves that go into harsh environments, to make sure they hold up.
At the end of the day, our whole process is about one thing: making sure the threaded valve you get from us works when you install it, no surprises. We’re not here to sell you a cheap valve that’ll cost you more in repairs later. We’re here to build long-term relationships, because that’s what this business is about. If you’re a contractor, a plumber, an industrial plant manager, anyone who needs reliable threaded valves, let’s chat. We can talk about your specific application—whether it’s residential HVAC, food and beverage lines, chemical processing, whatever—and make sure we test every valve exactly to your needs. No generic tests, no cutting corners, just parts that work when you need them.
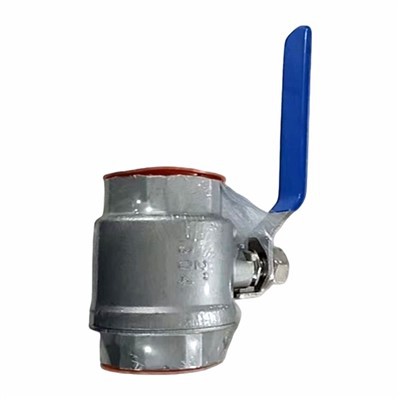
Wait, one last thing: if you’re testing valves on your end, don’t forget to document everything. Keep test reports, make a log of which batch passed which tests, so if something does go wrong (even though it won’t be our fault), you can track it back. That’s a good practice for everyone.
Butterfly Valve References:
- American National Standards Institute (ANSI) B1.20.1, Pipe Threads, General Purpose (American)
- American Water Works Association (AWWA) C507, Valves for Water Supply
- ISO 5208, Industrial valves – Pressure testing of metallic valves
- National Fire Protection Association (NFPA) 13, Standard for Installation of Sprinkler Systems
Xiongxiang Valve Group Co., Ltd.
As one of the most professional threaded valve manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to wholesale cheap threaded valve for sale here from our factory. Contact us for more details.
Address: Building 1, No.306, 12th Binhai Road, Jinkai District, Wenzhou City, Zhejiang Province, China
E-mail: info@xiongxiangvalve.com.cn
WebSite: https://www.steelvalvegroup.com/
