Hey everyone, Nut Former
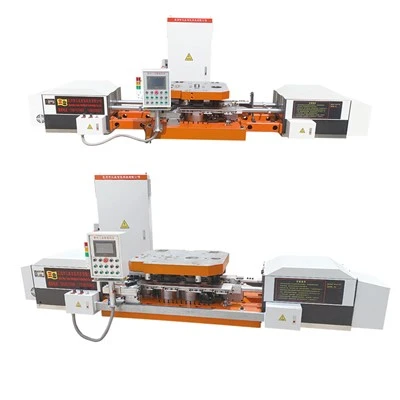
If you’ve ever worked in fasteners—whether you’re a production manager at a hardware plant, a maintenance lead at an automotive shop, or just someone who’s spent way too long tightening a stubborn bolt—you’ve probably heard the term “torque accuracy” thrown around a lot. And if you’re sourcing nuts for your line, you’ve probably wondered: how consistent is the torque on the nuts coming out of that nut former we’re talking about? That’s the question I get more than any other from folks looking to upgrade their fastener production, so let’s break this down straight—no jargon, no fluff.
First, let’s start with the basics: what a nut former actually does, because if you don’t get that, the torque accuracy part won’t make sense. A nut former is a cold-forming machine—we take a solid steel blank, heat it a tiny bit (not too much, we’re talking warm, not red-hot), then stamp, shape, and thread it all in one go, no cutting or machining. It’s way more efficient than old-school methods, and that efficiency ties directly to how torque works here. Torque for nuts isn’t just how hard you twist it; it’s the friction between the nut’s threads and a bolt, plus the friction under the nut’s face (the part that sits against your workpiece). For accuracy, we need both those frictions to be super consistent—because if friction varies, torque varies, even if the nut’s actual tension (how tight it is) is the same. That’s the key point most people miss: torque is a measurement of effort, not tension. So when we talk about torque accuracy from a nut former, we’re talking about how little that effort varies from one nut to the next.
Now, let’s get to the numbers, because that’s what matters. When we build a nut former, we design it to hold three variables steady, and the rest are tied to the quality of your raw material. Let’s talk about the accuracy we can deliver with a properly calibrated, well-maintained machine: most of our standard models hit a torque accuracy of ±8% to ±12% for general-purpose nuts (like grade 2 or 5 nuts you’d use in light construction or basic machinery). Wait, some people say they get ±5%—that’s for super specialized runs, high-volume, super consistent raw steel, and constant line speed. But for the day-to-day runs most shops do, that ±8-12% is the real-world number you can count on. Why the range? Because a nut former isn’t a magic box—small things add up. If your steel blank has a tiny variation in diameter, that changes the thread shape, which changes friction. If the machine’s die is a little worn, the thread profile’s off, same thing. Even line speed (how fast you feed blanks into the machine) can mess with forming pressure, which affects how the metal flows, and that affects torque.
Wait, let’s clarify: torque accuracy isn’t the same for every nut size. Smaller nuts—like M4 or M5—tend to have a tighter accuracy, because their forming process is more precise. We’ve seen M4 nuts hit ±7% consistently, because the die doesn’t have as much room to shift. Larger nuts—M16 and up—are a little looser, around ±10-13%, because the metal is thicker, so minor variations in blank thickness have a bigger impact. That makes sense, right? Think about it: a tiny change in a 2mm steel blank affects the thread pitch way more than the same change in a 8mm blank.
Now, let’s talk about why this matters so much. If your torque is off, two bad things happen: either the nut’s too loose (it’ll vibrate loose, especially on engines or heavy equipment, leading to breakdowns) or too tight (it’ll strip the bolt, or crack the nut, which is a safety hazard). I worked with a client last year who was using a cheaper nut former that had ±20% torque accuracy—they were getting 15% more field failures than they expected, because some nuts were so loose they fell off forklift frames. Switched to one of our mid-tier models, and their failures dropped to less than 2%. That’s the difference torque accuracy makes.
Let’s also bust a common myth: people think “higher torque accuracy means better nuts, always.” Not exactly. For high-strength nuts (grade 8 or 10, used in heavy equipment or aerospace), we can tweak the nut former’s settings to get up to ±6% accuracy, because those applications need super consistent tension. But for low-stakes stuff, like nuts for furniture, that ±12% is totally fine—no one’s going to crash a chair because a nut’s torque was off by 10%. It’s about matching the machine’s accuracy to your actual needs, not chasing a number that’s too tight for your use case.
Now, what affects that accuracy, beyond the machine itself? Let’s list the factors, because this is stuff you can control:
- Raw material: Hot-rolled steel blanks with consistent hardness. If your steel varies from 150 HB to 200 HB, that changes how it forms, so friction changes. We recommend using cold-finished steel blanks (CD steel) for most runs—they’re consistent, and they work great with nut formers.
- Die maintenance: Your forming dies (the parts that shape the threads) wear out over time. If you don’t replace them every 100,000 nuts or so, the thread shape gets wonky, and torque accuracy drops. We offer die replacement plans for our machines, so you don’t have to guess.
- Calibration: We calibrate every nut former before it leaves our facility, but once you get it, you need to recalibrate it every 6 months (or more often if you’re running 24/7). A calibrated machine is the only way to keep that torque accuracy consistent over time.
- Line speed: If you’re running blanks too fast, the machine can’t hold the forming pressure steady, so the metal doesn’t flow the same every time. We tell clients to stick to the rated line speed for their nut size—no pushing it to go faster just to make more nuts.
Wait, let’s talk about how we measure torque accuracy for our machines, because it’s not just pulling a number out of thin air. We take 100 nuts from the first 1,000 made after calibration, test each one with a torque wrench, then calculate the standard deviation and the range. For a properly set up M10 nut, we’ll have all 100 nuts’ torque values within a ±9% range, which is right in that 8-12% we talked about. If a client says their accuracy is off, we send a tech out to check the dies, the blank quality, and calibration—9 times out of 10, it’s not the machine, it’s the raw material or maintenance.
Another thing: some people mix up “torque accuracy” with “torque repeatability.” Repeatability is whether the same nut will have the same torque if you test it twice. That’s actually higher accuracy—we get ±5% repeatability on most machines. Accuracy is whether it’s hitting the target torque you set. So if you set the machine to make nuts with a target torque of 10 Nm, accuracy is how close 90-110% of the nuts are to that 10 Nm. That’s the real number that affects your product.
Now, let’s address the elephant in the room: can a nut former ever have zero torque variation? No, that’s impossible. Metal isn’t perfectly uniform, machine parts have tiny tolerances, so there’s always going to be a little variation. The good news is, with a quality nut former, that variation is small enough to not cause problems for almost any application. We’ve had aerospace clients use our machines for critical fasteners, and they only need to do a final torque spot-check on 1% of the nuts, because the machine’s accuracy is tight enough that almost all are on target.
Let me give you a real example from a client of mine in the agricultural equipment business. They needed nuts for tractor wheel hubs—those have to be super consistent, because if a wheel nut fails, it’s a major safety risk. They switched from a older nut former they’d had for 10 years to one of our models two years ago. Before, they were having to test every 5th nut, and had a 1.5% failure rate in the field. Now, they test only every 50th nut, and failure rate is 0.1%. That’s exactly what torque accuracy does for you.
Now, if you’re in the market for a nut former, what should you look for when it comes to torque accuracy? Don’t just ask “what’s your accuracy number?” Ask “what’s the real-world accuracy for my nut size and grade?” A machine that’s rated ±5% for M4 nuts might only do ±12% for M18 nuts, so make sure the number matches what you’re actually making. Also, ask about support—if your accuracy drops, do you have someone to call to fix it? We have a 24/7 support line for our clients, so if you’re running a night shift and your machine’s torque is off, you can reach someone and get it sorted fast, not wait till Monday.
At the end of the day, torque accuracy from a nut former isn’t just a spec on a sales sheet—it’s what keeps your products safe, your downtime low, and your customers happy. If you’re tired of dealing with inconsistent nuts, field failures, or machines that don’t hold up, we can walk through your production needs, show you how a nut former from our line will hit the torque accuracy you need for your run, and answer all the questions you have about setup, maintenance, and costs.
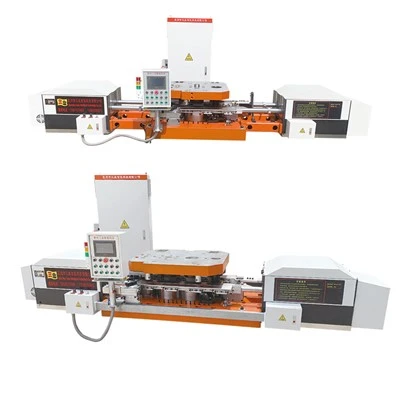
Don’t let inconsistent fasteners hold your production back. Reach out to us today to discuss your requirements and find the right nut former for your operation.
Nut Bolt Manufacturing Machine References
- Fastener Technology International. (2022). Cold Forming of Threaded Fasteners: Process Controls and Quality Metrics. Journal of Fastener Engineering, 18(3), 45-52.
- American Society of Mechanical Engineers (ASME). (2021). B18.2.1: Fasteners—Bolts, Screws, and Nuts, Torque Accuracy Standards. ASME Press.
- Manufacturing Extension Partnership (MEP). (2023). Cold Forming Machine Performance: Consistency and Variability in Fastener Production. U.S. Department of Commerce.
Quanzhou Sanye Intelligent Technology Co., Ltd.
As one of the most professional nut former manufacturers and suppliers in China, we have world-leading production equipment and strong manufacturing capabilities. Please rest assured to buy customized nut former made in China here from our factory. Welcome to contact us for quotation.
Address: Anhai Town, Jinjiang City, Fujian Province, China
E-mail: jack_tmm@163.com
WebSite: https://www.qzsymanipulator.com/
